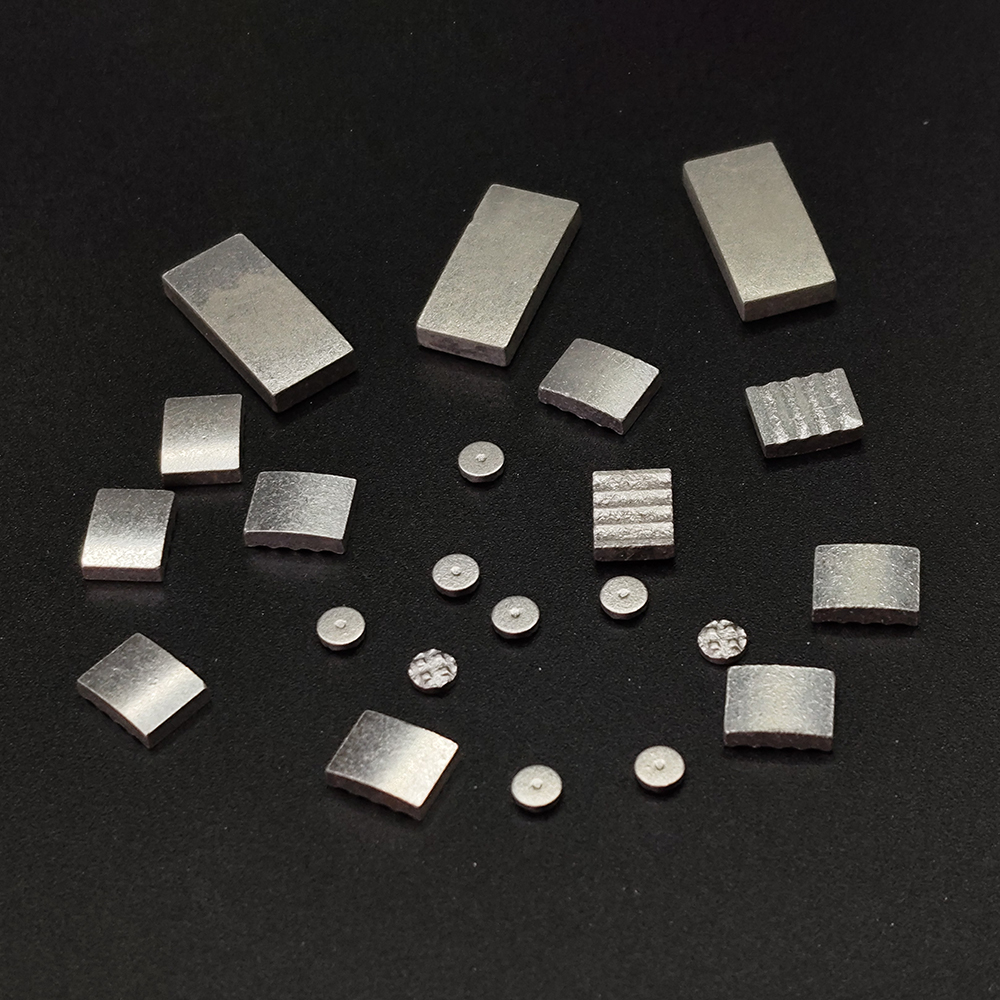
Silver Alloy Wire Contact Products for MCBs
Our precision-engineered silver alloy wire-based contact products are specifically designed for medium-to-high current miniature circuit breakers, ensuring reliable switching performance and extended operational life.
What Are Silver Alloy Wires for Medium-to-High Current MCBs?
Silver alloy wires represent a cornerstone material in the manufacture of electrical contacts for miniature circuit breakers (MCBs) operating under medium-to-high current conditions — typically ranging from 16A to 125A and beyond. These precision-drawn wires are produced from optimized silver-based alloy compositions such as AgSnO₂, AgSnO₂In₂O₃, AgNi, AgZnO, and AgCu, each engineered to deliver specific electrical, thermal, and mechanical performance attributes.
In the context of MCBs, the contact wire serves as the raw feedstock for manufacturing contact tips, rivets, and bimetal assemblies. The wire is cold-drawn to exact dimensional tolerances, with composition and microstructure carefully controlled to ensure consistent contact resistance, arc erosion resistance, and welding resistance — all critical parameters for safe and reliable circuit protection.
As global electrical infrastructure evolves toward smarter grids, renewable integration, and higher-power distribution demands, the performance requirements for MCB contact materials have increased significantly, making advanced silver alloy wires indispensable.
Why Silver Alloy Wires Are Critical for High-Performance MCBs
In medium-to-high current MCB applications, contacts must reliably interrupt fault currents often exceeding 10kA, withstand thousands of make-and-break operations, resist contact welding, and maintain stable contact resistance across their service life. Standard silver or copper contacts cannot meet these combined demands. Only precision-engineered silver alloy wires — with optimized oxide dispersions and alloying elements — can deliver the arc quenching capability, erosion resistance, and thermal management required for safe, long-life circuit protection.
Key Performance Features of Silver Alloy Wires in MCBs
Superior Arc Erosion Resistance
Silver alloy wires — especially AgSnO₂ compositions — exhibit outstanding resistance to arc erosion during repeated fault current interruptions, ensuring contact mass integrity across tens of thousands of switching cycles in medium-to-high current MCBs.
Anti-Welding Performance
Contact welding is a primary failure mode in high-current MCBs. Silver alloy wires with dispersed oxide phases provide a physical barrier that prevents micro-welding at contact interfaces, even under severe short-circuit conditions.
Tight Dimensional Tolerances
Precision cold-drawing processes achieve wire diameters with tolerances as tight as ±0.005mm, enabling automated contact stamping and riveting in high-speed MCB assembly lines with minimal reject rates.
Thermal Stability
Engineered alloy microstructures maintain stable oxide dispersion and grain structure at elevated temperatures, ensuring consistent contact resistance and mechanical strength even during prolonged overload conditions.
High Electrical Conductivity
Optimized alloy compositions retain high bulk electrical conductivity — typically 70–85% IACS for AgSnO₂ — minimizing contact heating and energy losses in high-current MCB applications, contributing to system efficiency.
Eco-Friendly Composition
Modern silver alloy wire formulations are free from cadmium and other hazardous materials, complying with RoHS, REACH, and international environmental regulations — an increasingly critical requirement for global MCB manufacturers.
Silver Alloy Wire Compositions for MCB Applications
Different current levels and switching duties demand tailored alloy compositions. The table below summarizes the principal silver alloy wire types used in medium-to-high current MCB contacts and their primary performance characteristics.
| Alloy Type | Typical Composition | Key Advantage | Best MCB Application |
|---|---|---|---|
| AgSnO₂ | Ag + 8–12% SnO₂ | Excellent arc erosion & anti-weld | High-current MCBs (40A–125A) |
| AgSnO₂In₂O₃ | Ag + SnO₂ + In₂O₃ | Enhanced conductivity & erosion life | Medium-to-high current (25A–100A) |
| AgNi | Ag + 10–30% Ni | Low contact resistance, easy processing | Medium current MCBs (16A–63A) |
| AgZnO | Ag + 5–10% ZnO | Good arc quenching, cost-effective | Medium current applications (16A–50A) |
| AgCu | Ag + 10–30% Cu | High hardness, wear resistance | Heavy-duty MCB contacts (40A–125A+) |
Deep-Dive: Where Silver Alloy Wires Are Used in MCB Systems
Silver alloy wires for MCBs extend far beyond simple residential circuit protection. Their use spans critical industrial, commercial, and energy infrastructure applications where reliable overcurrent protection is paramount.
Industrial Motor Protection MCBs
High-current MCBs protecting motor feeders (40A–125A) experience frequent inrush currents and must handle both overload and short-circuit conditions. AgSnO₂ wire-based contacts withstand the severe arc energy of motor fault interruption without welding or excessive erosion, ensuring reliable tripping and long maintenance intervals in demanding factory environments.
Commercial Building Distribution Panels
Modern commercial buildings deploy dense arrays of MCBs in distribution boards protecting HVAC, lighting, and power circuits at 32A–100A ratings. Silver alloy wire contacts in these MCBs must maintain consistent performance across thousands of normal switching operations and occasional fault events over decades of service, with minimal maintenance access.
Solar PV & Renewable Energy Systems
Photovoltaic string combiner boxes and inverter protection require MCBs with DC-rated contacts capable of arc interruption without zero-crossing — a far more challenging duty than AC switching. AgSnO₂In₂O₃ wire contacts deliver the sustained arc resistance needed for reliable DC circuit protection in solar installations operating at 1000V DC and currents up to 125A.
EV Charging Infrastructure
Level 2 and DC fast-charging stations demand MCBs with exceptional short-circuit breaking capacity and anti-weld performance, as EV charging introduces complex load profiles with high instantaneous currents. Silver alloy wire contacts engineered for EV protection MCBs are emerging as a key enabler of safe, high-throughput charging infrastructure.
Critical Facility Power Systems
Hospitals, data centers, and telecommunications facilities require MCBs with zero-compromise reliability. Silver alloy wire contacts in these applications must deliver predictable tripping characteristics throughout a 15–20 year service life, as unexpected contact failure or nuisance tripping can have severe safety and operational consequences.
Rail & Transportation Power Distribution
Railway auxiliary power systems, trackside equipment, and onboard rolling stock use MCBs subject to vibration, wide temperature swings, and high short-circuit currents. AgCu and AgSnO₂ wire contacts are preferred for their combination of mechanical robustness, arc interruption capability, and stable contact resistance in these challenging environments.
Industry Trends Driving Demand for Advanced Silver Alloy Wire MCB Contacts
The global MCB market is undergoing rapid transformation, driven by electrification, digitalization, and sustainability imperatives. These macro-trends are reshaping material performance requirements and creating new growth opportunities for high-performance silver alloy wire solutions.
📈 Surging Global MCB Market
The global miniature circuit breaker market was valued at over USD 5 billion in 2023 and is projected to grow at a CAGR exceeding 6% through 2030. This growth is fueled by accelerating urbanization, expanding industrial automation, renewable energy deployment, and EV infrastructure buildout — all requiring high-quality MCB contact materials.
🌱 Cadmium-Free Material Transition
Regulatory pressure under RoHS and REACH directives has accelerated the global transition from AgCdO contacts to cadmium-free alternatives. AgSnO₂ and AgSnO₂In₂O₃ wire materials have become the preferred replacement, with ongoing R&D focused on further improving their performance to fully match or exceed legacy AgCdO in all current classes.
⚡ Higher Breaking Capacity Requirements
As grid short-circuit levels increase due to distributed generation and denser interconnection, MCBs must achieve higher ultimate breaking capacities (Icu) — often 10kA to 25kA at rated voltage. This pushes contact material performance envelopes, demanding silver alloy wires with optimized arc erosion properties and superior anti-weld characteristics.
🔌 DC Circuit Protection Expansion
The proliferation of DC microgrids, battery energy storage systems, and EV infrastructure is creating entirely new categories of MCB applications. DC circuit interruption presents fundamentally different arc physics compared to AC, requiring silver alloy wire compositions and geometries specifically optimized for reliable arc quenching without a natural current zero.
🤖 Automation-Driven Precision Requirements
High-speed automated MCB assembly lines require silver alloy wires with extremely consistent diameter tolerances, surface finish, and mechanical properties to minimize tooling wear and reject rates. This is driving adoption of advanced wire drawing technologies and rigorous in-process quality monitoring, raising the bar for wire supplier capabilities.
🌍 Localization & Supply Chain Resilience
Post-pandemic supply chain disruptions have prompted major MCB manufacturers in Europe, North America, and Southeast Asia to diversify their silver alloy wire sourcing. This creates opportunities for technically capable suppliers with both the material expertise and production reliability to become qualified second or primary sources for leading MCB brands.
Company Profile
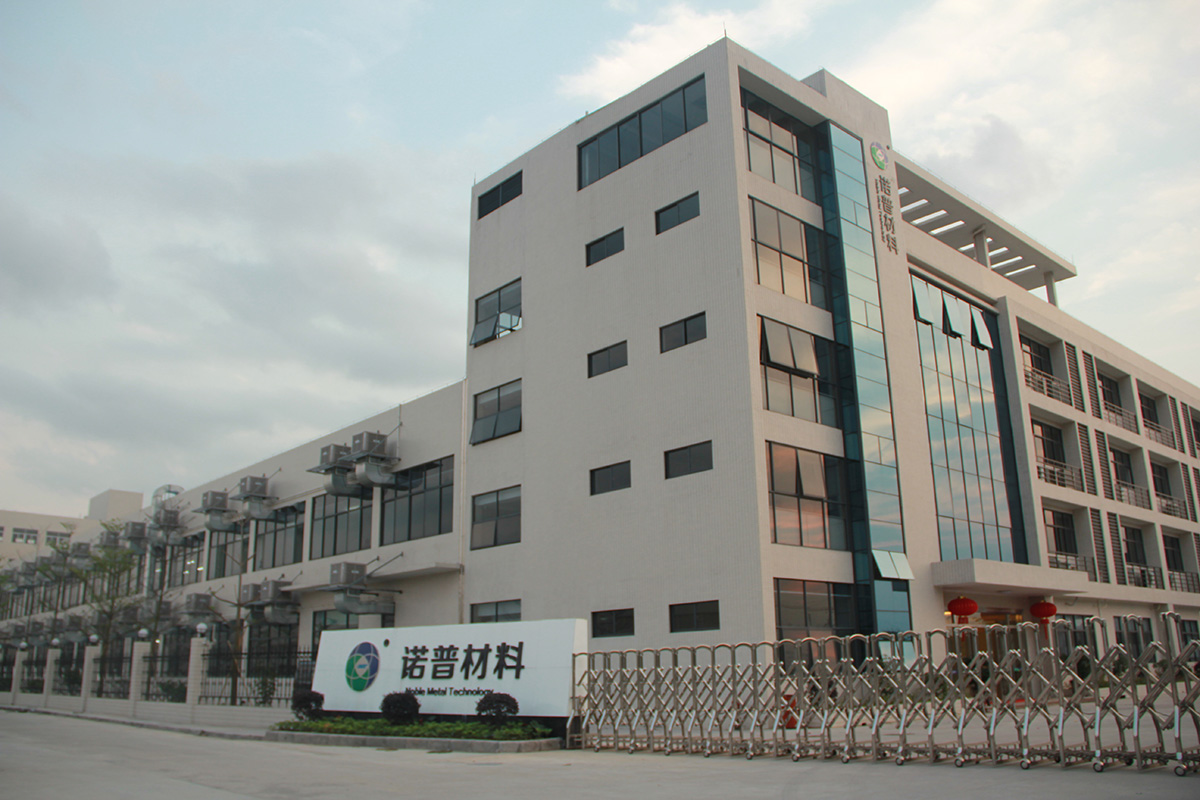
Foshan Noble Metal Technology Co., Ltd. (known as NMT) is a leading high-tech enterprise specializing in the development and manufacture of silver-based electrical contact composite materials, components and assemblies for various electrical and electronic applications. Our headquarter is located in Foshan with state-of-the-art facilities.
As a trusted partner to global MCB manufacturers, NMT brings decades of silver alloy expertise to every product — from raw wire feedstock to finished contact assemblies. Our deep understanding of MCB switching physics, combined with advanced metallurgical capabilities, enables us to develop tailored silver alloy wire solutions that meet the evolving performance demands of medium-to-high current circuit breaker applications worldwide.
Professional Certificates
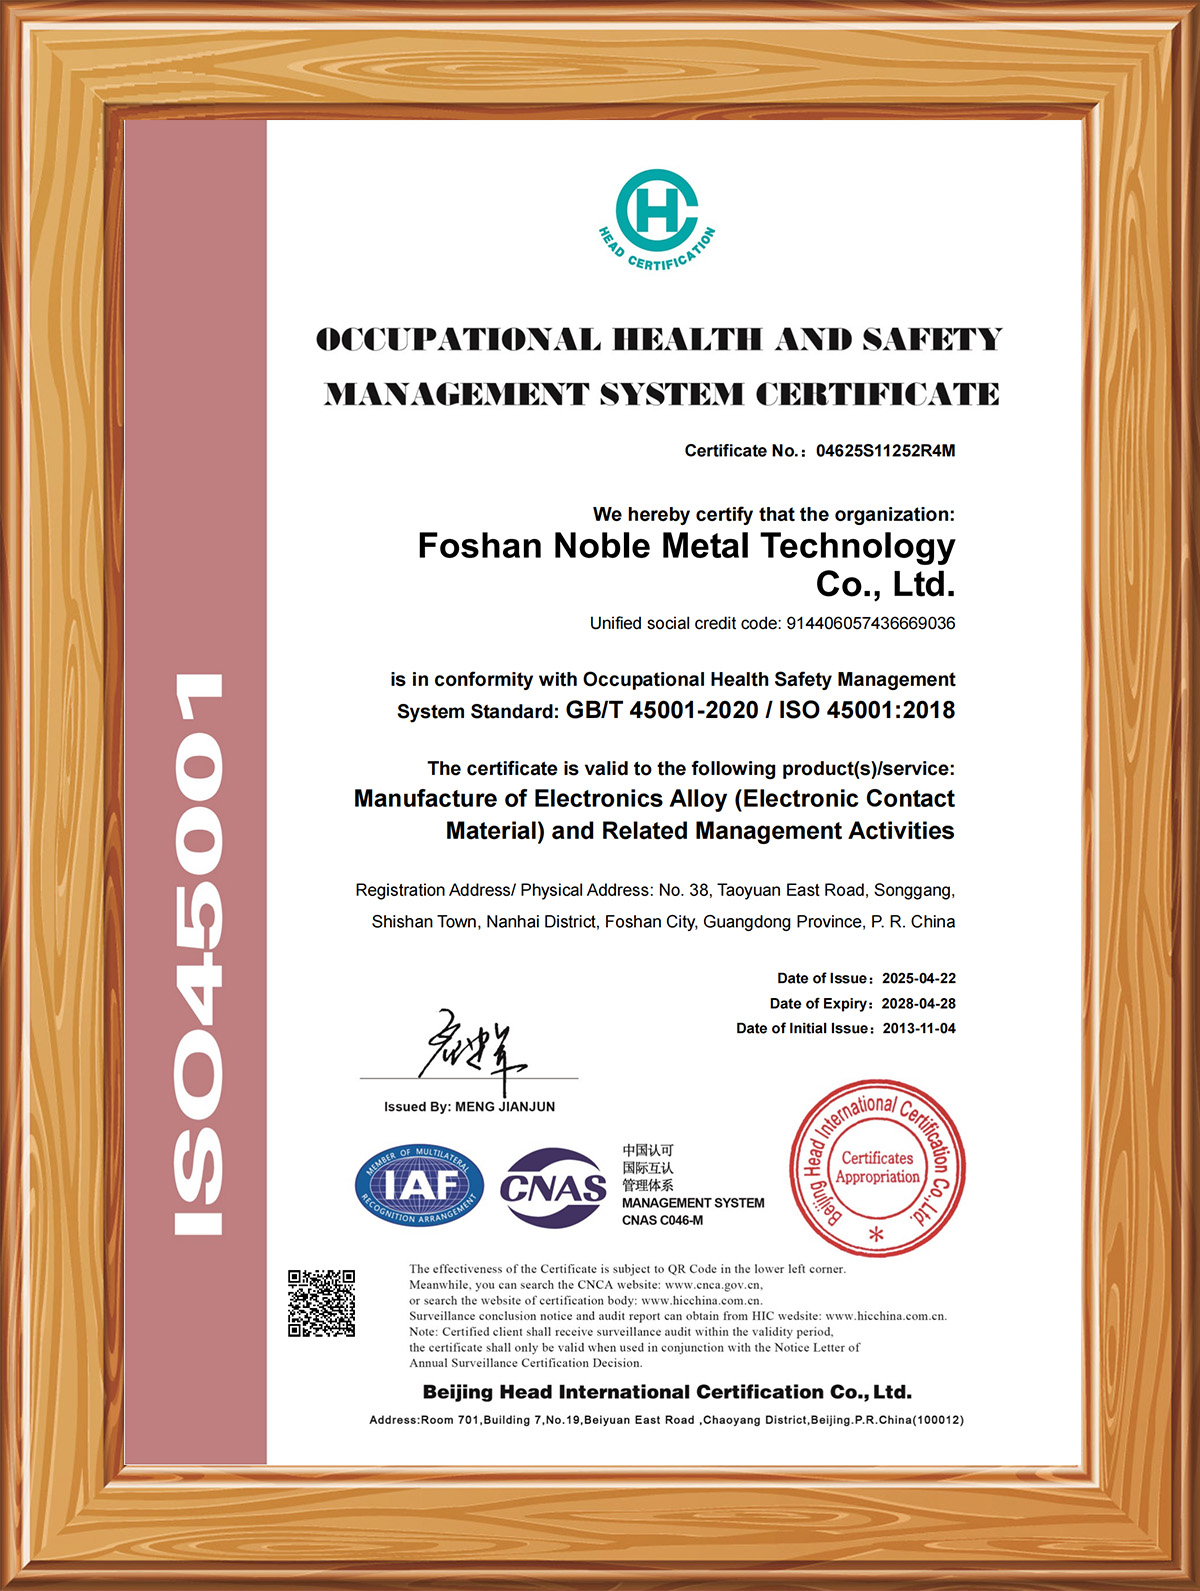
NMT has obtained the National Invention Patent of "AgSnO₂In₂O₃ electric contact composite material and its manufacture processes" in 2008. Through our expert know-hows and strong technical team, NMT has further developed AgSnO₂ alloy materials with different compositions and innovative processes, which results in better performance and broader range of applications. Additionally, NMT has also developed various ranges of silver-based electrical contact materials such as AgNi, AgZnO, and AgCu etc., which may offer our customers more options in their applications.
Quality Control
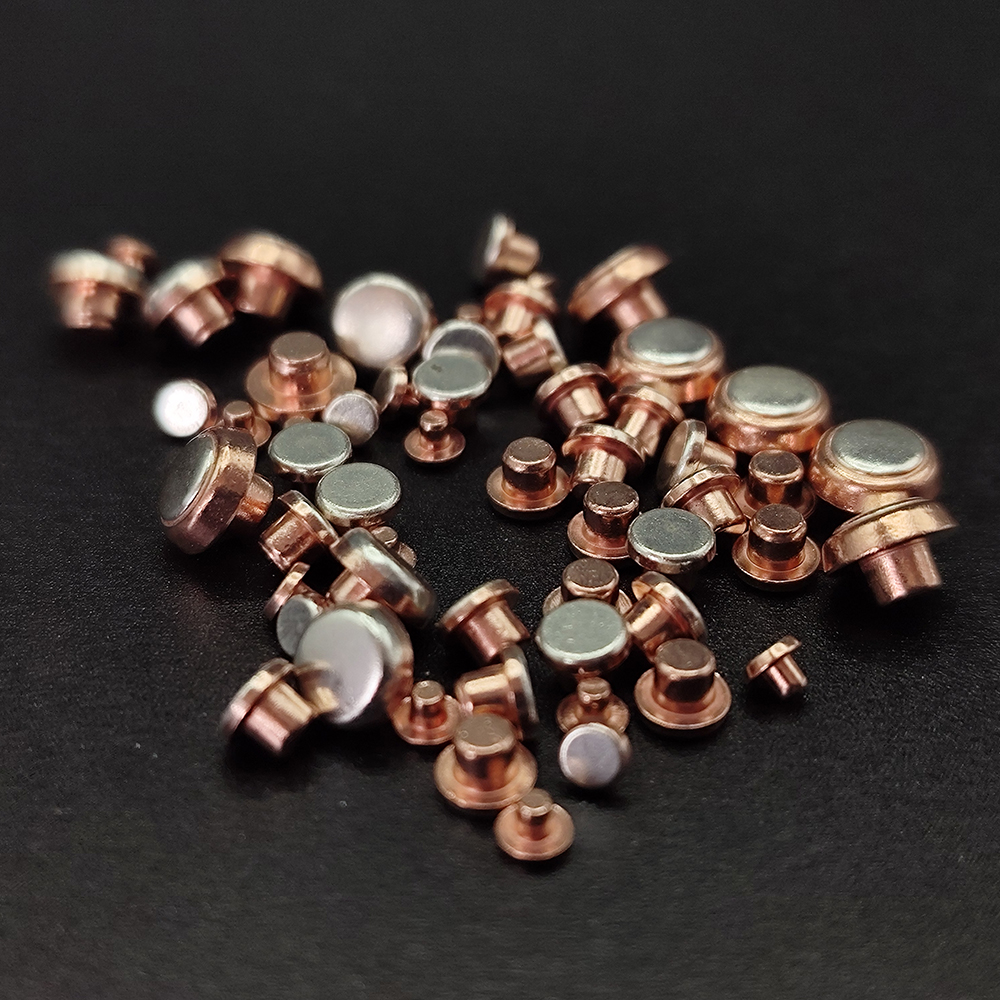
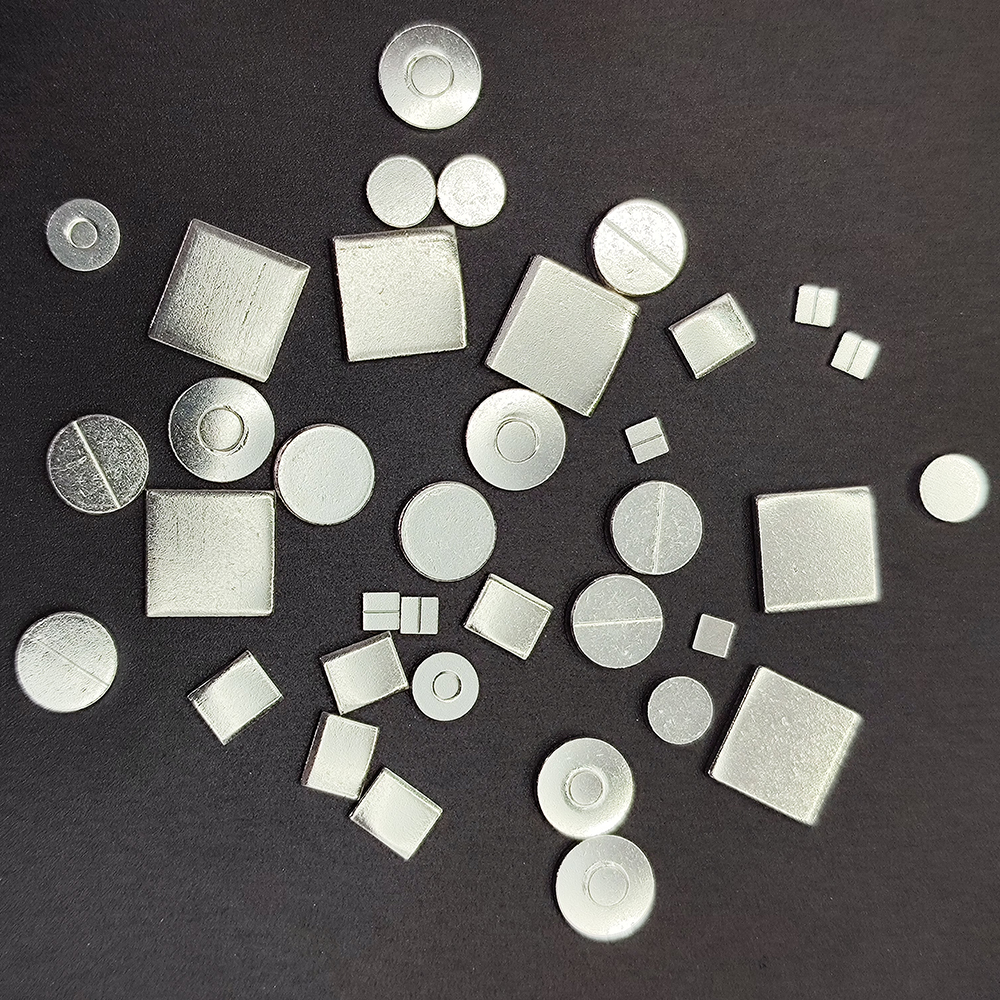
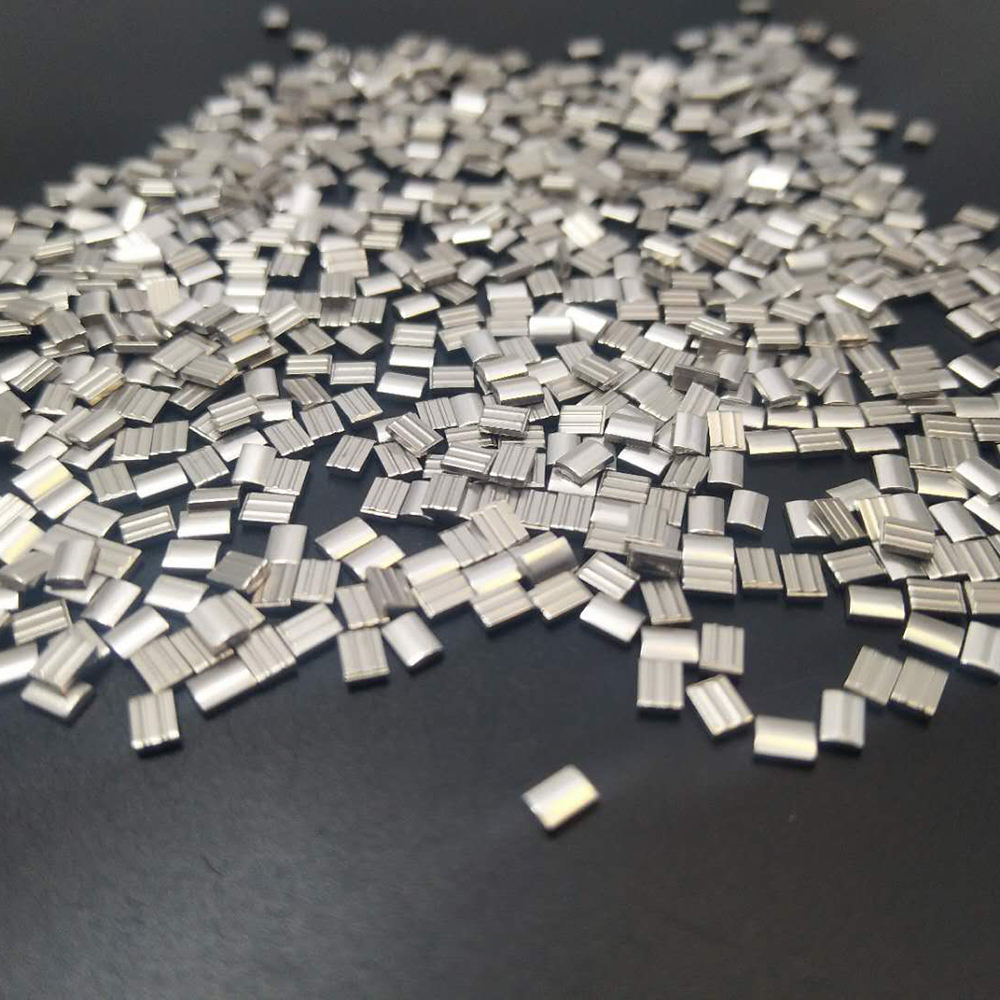
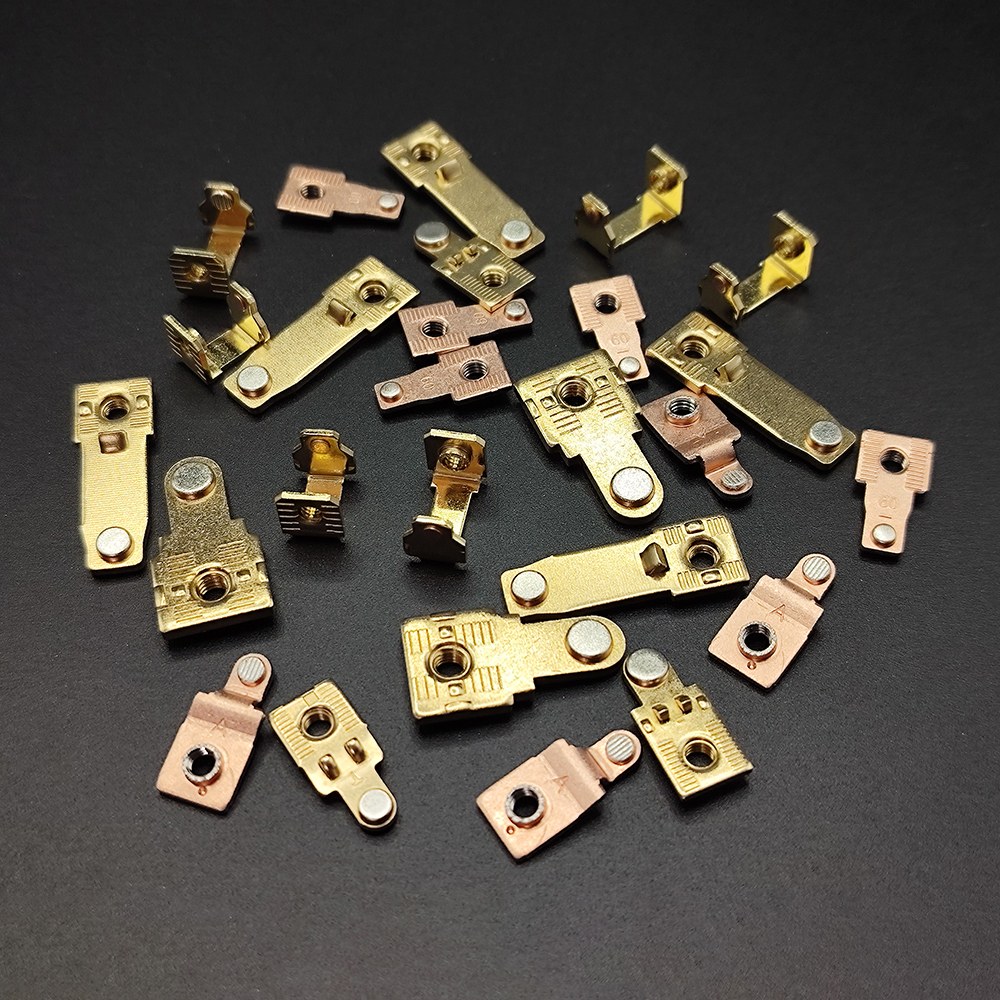
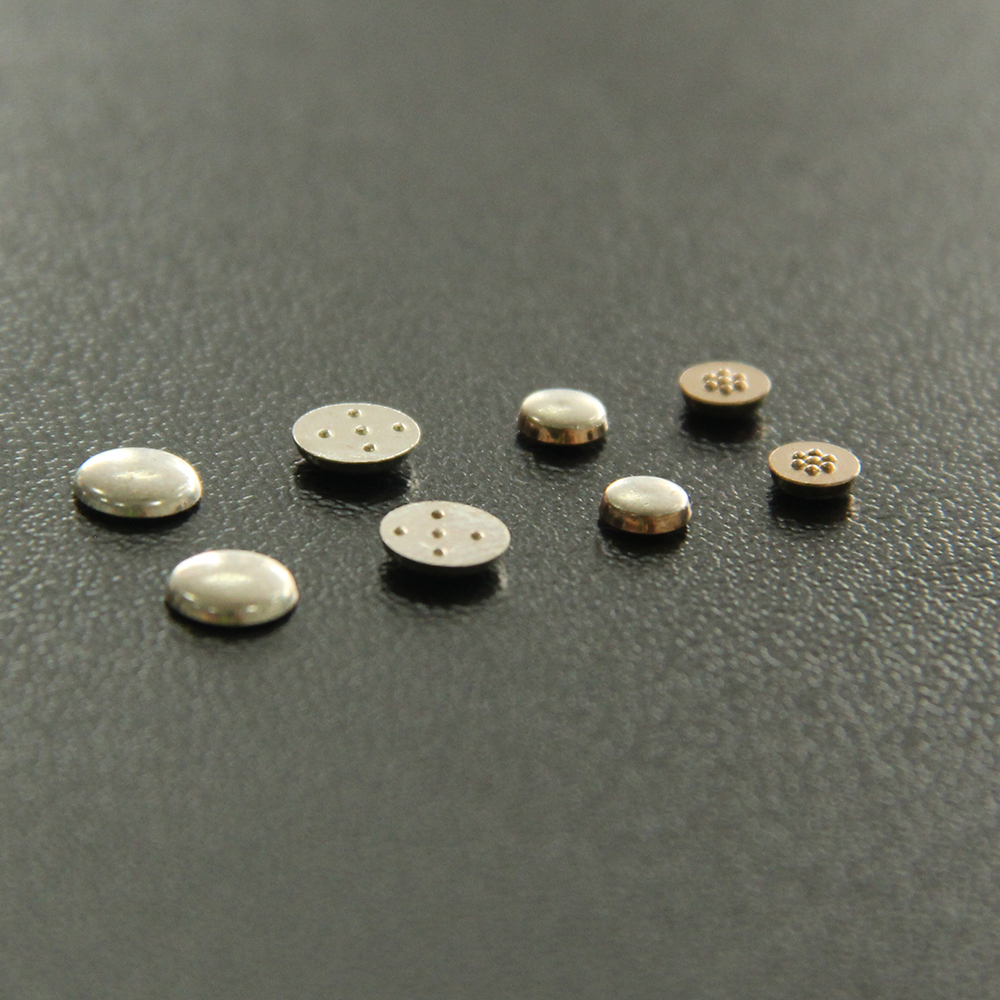
Our business covers a wide range of areas, including contact materials in the form of powder, wire, composite strip, and profiles. We also offer contact components, such as tips and rivets, and contact assemblies, which include welded and stamped components. In addition, we have a series of silver paste products.
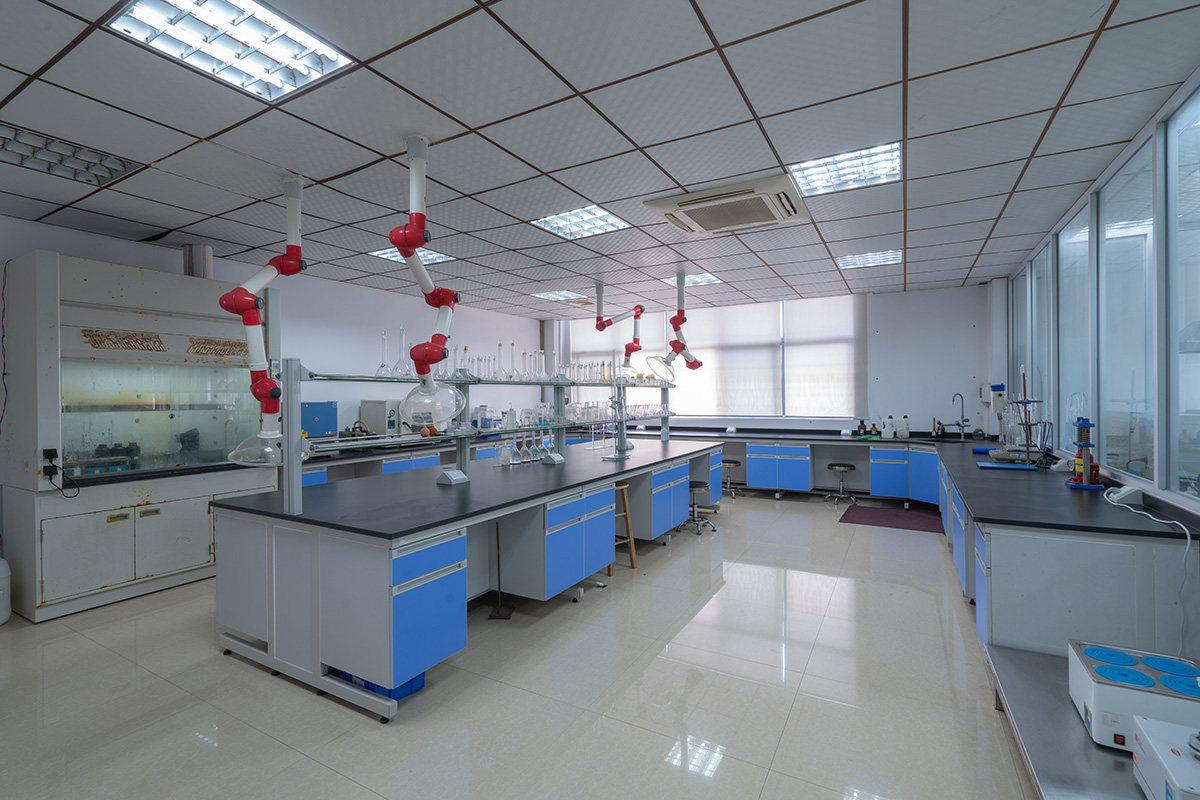
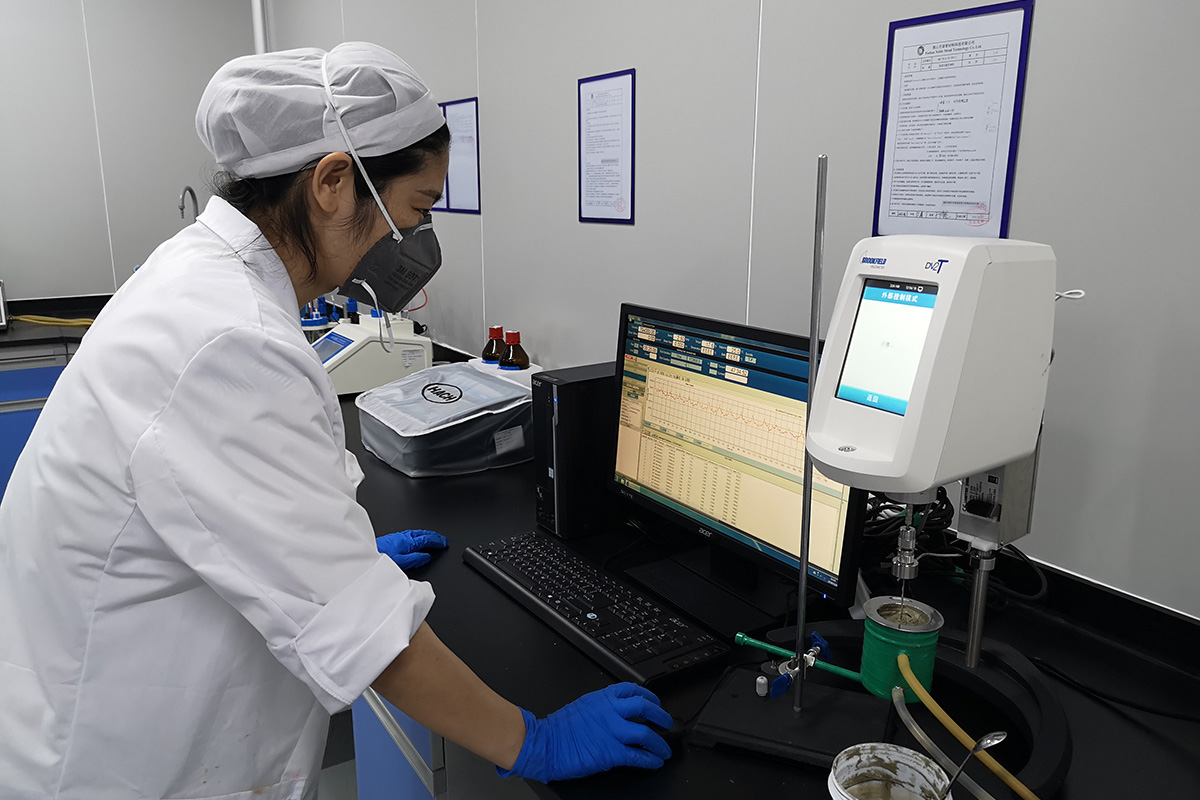
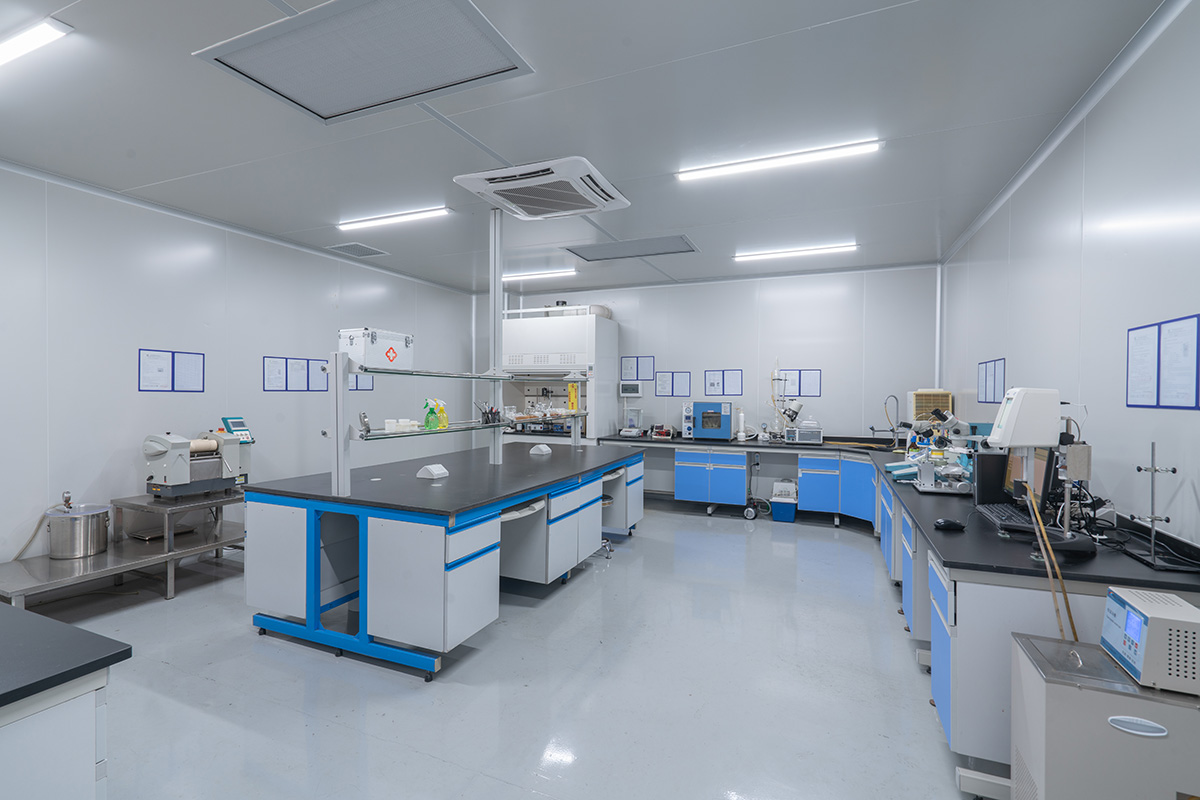
These comprehensive offerings enable us to provide our customers with integrated and cost-effective solutions while ensuring complete manufacturing and quality control. For silver alloy wire products destined for MCB contact manufacturing, our quality system enforces 100% dimensional inspection, resistivity verification, hardness testing, and microstructural analysis at every production stage.
Every batch of silver alloy wire shipped to MCB manufacturers is accompanied by full material certifications, traceability documentation, and test reports — providing the assurance that high-volume automated assembly processes demand.
Innovative R&D
NMT has kept investing in R&D and following up the most up-to-date techniques and applications via cooperation and exchange with customers and research organizations, which drive NMT to deliver more innovative, eco-friendly, and high-quality solutions to our customers.
We continually strive to enhance our products, expand our capabilities, and improve our manufacturing processes. By doing so, we can continue to provide our customers with cutting-edge solutions to meet the changing needs. NMT is a trusted supplier of silver-based electrical contact materials, components, and assemblies. With our strong technical team, broad product range, and commitment to innovation, we have the ability to provide customers with integrated and reliable solutions.
Silver Alloy MCB Contact Product Series
From wire-drawn contact rivets to precision-stamped assemblies, our complete silver alloy product portfolio supports every stage of MCB contact component manufacturing.


Partner with NMT for Advanced Silver Alloy Wire MCB Solutions
Whether you need standard AgSnO₂ wire for established MCB designs or a fully customized silver alloy formulation for next-generation high-current circuit breakers, our technical team is ready to collaborate. Contact us today to discuss your specifications and discover how NMT's silver alloy wire expertise can enhance your MCB product performance.
Request a Technical Consultation